

Simulation ensures material flow in chocolate biscuit production
Food manufacturer: Buffers and storage to counter disruptions in packaging
A manufacturer of chocolate biscuits was planning a completely new production line – from dough preparation through the oven and chocolate coating (single-bar system) to packaging and palletising. Systems of this scale involve an investment of around €20 million. As a stoppage in one part of the plant immediately affects all the others, the company used simulation to validate the design before awarding the contract: plant efficiency of over 95 per cent instead of around 85 per cent, around 10 per cent less raw material loss, and storage facilities 40 per cent smaller – with simulation costs amounting to less than 0.2 per cent of the investment sum.
The project in figures
| Key figure | Value |
|---|---|
| Investment volume of the protected plant | In the region of €20 million |
| Simulation effort | Less than 0.2% of the investment volume |
| Project duration | Around 3 months |
| Plant efficiency | From around 85% to over 95% |
| Avoidable raw material loss | Around 10% of the target volume |
| Required buffer capacity | Around 40% lower than planned |
Initial situation: Disruptions in the packaging process affect the entire line
Production and chocolate coating are continuous processes with long lead times: product that is, or would be, stuck in the oven or in the cooling sections during a stoppage is lost and must be discharged. Packaging, on the other hand, operates discontinuously and accounts for most short stoppages – film roll changes, replenishing magazines, inspection cycles. This makes it the critical part of the system: any build-up that carries through to the oven costs not only time but also raw materials.
Objective: Identify knock-on effects early and design storage correctly
- Position and size buffers between production and packaging in such a way that brief stoppages are absorbed – without investing in oversized buffers
- Develop a control logic that links the plant components via buffer levels, rather than simply decoupling them mechanically
- Determine the economic operating point and the expected plant efficiency as reliable planning parameters
Solution: Simulation model of the entire process chain
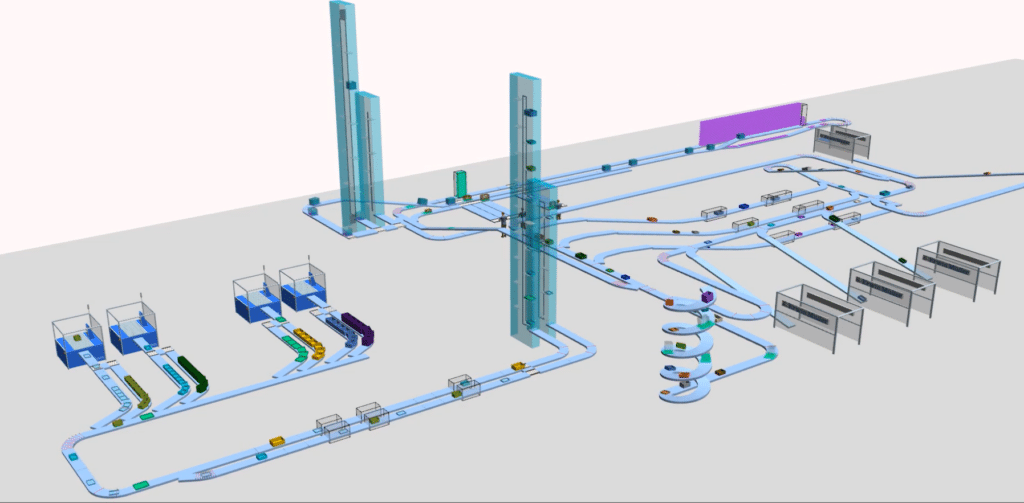
SimPlan modelled the end-to-end material flow from the dough batch to the wrapped pallet – including availability and average repair times for every element relevant to throughput, as well as stochastically generated disruptions. Following validation against the planned nominal capacity, over 30 experiments were conducted, each with four weeks of simulated operating time, totalling more than two years of virtual production.
A key factor was level-dependent storage control: the packaging buffers regulate the cycle rate of the chocolate moulding process, whilst the level in the intermediate buffer upstream controls the feed to the oven. The line slows itself down before a backlog develops – rather than discarding already baked products.
Results: A robust plant with reliable design data
Around 10% of raw material loss was prevented. At full rated capacity, the oven feed had to be forcibly shut off over 200 times in four weeks – averaging around one hour of downtime per shift. At the determined operating point, this practically ceased to occur, whilst pallet output remained virtually unchanged: the line delivers the same quantity of finished goods using significantly less raw material.
The plant’s efficiency rose from around 85 per cent to over 95 per cent. In the initial design, approximately 5 per cent of the target output was lost during production and around 10 per cent due to interactions between the chocolate moulding process and packaging.
The buffers could be designed to be around 40 per cent smaller. The smaller storage variant achieves the same throughput and the same efficiency; the plant’s speed reserves fully compensate for the more frequently reached capacity limits. The larger variant would have remained ineffective.
The economically optimal operating point lies a good 10 per cent below the rated capacity. Above this point, losses increase disproportionately because the furnace feed has to shut off more frequently. A targeted improvement in availability at just two key stations further boosted efficiency by over 5 percentage points – a strong argument for negotiations with the plant suppliers and a priority list for maintenance.
Why end-to-end simulation matters for combined process and packaging plants
Buffers alone do not solve the problem. They only work if the control system uses their fill levels to slow down the upstream processes in good time. Where this coupling is lacking, even the largest storage tank is of no help – where it works, a significantly smaller one is often sufficient. Both can only be determined through simulation prior to construction. This applies to manufacturers of chocolate products as well as to other companies with multi-stage production and packaging lines.